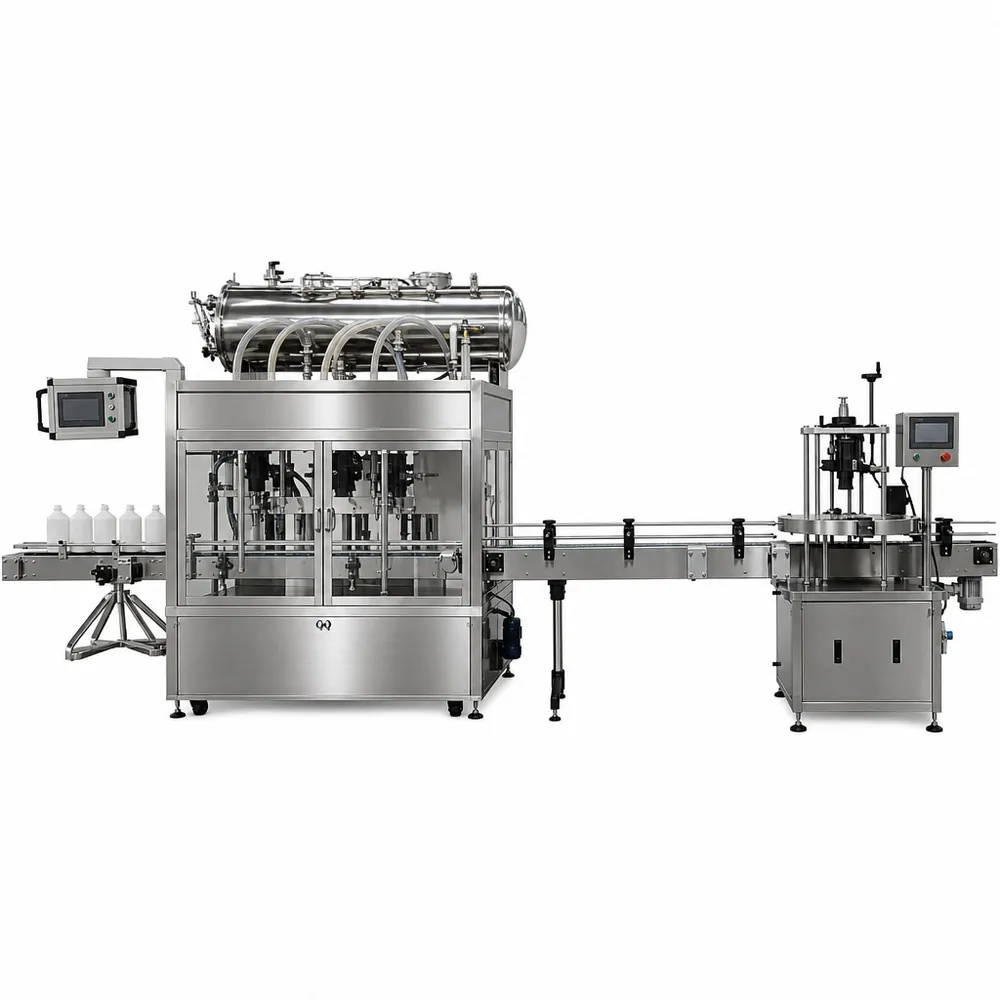
AT-01 Automatic Bottle Filling Machine — Piston
AT-01 uses a servo piston tracking arrangement in which filling nozzles follow containers along the conveyor.
View details →Equipment by application
AT-01 uses a servo piston tracking arrangement in which filling nozzles follow containers along the conveyor.
View details →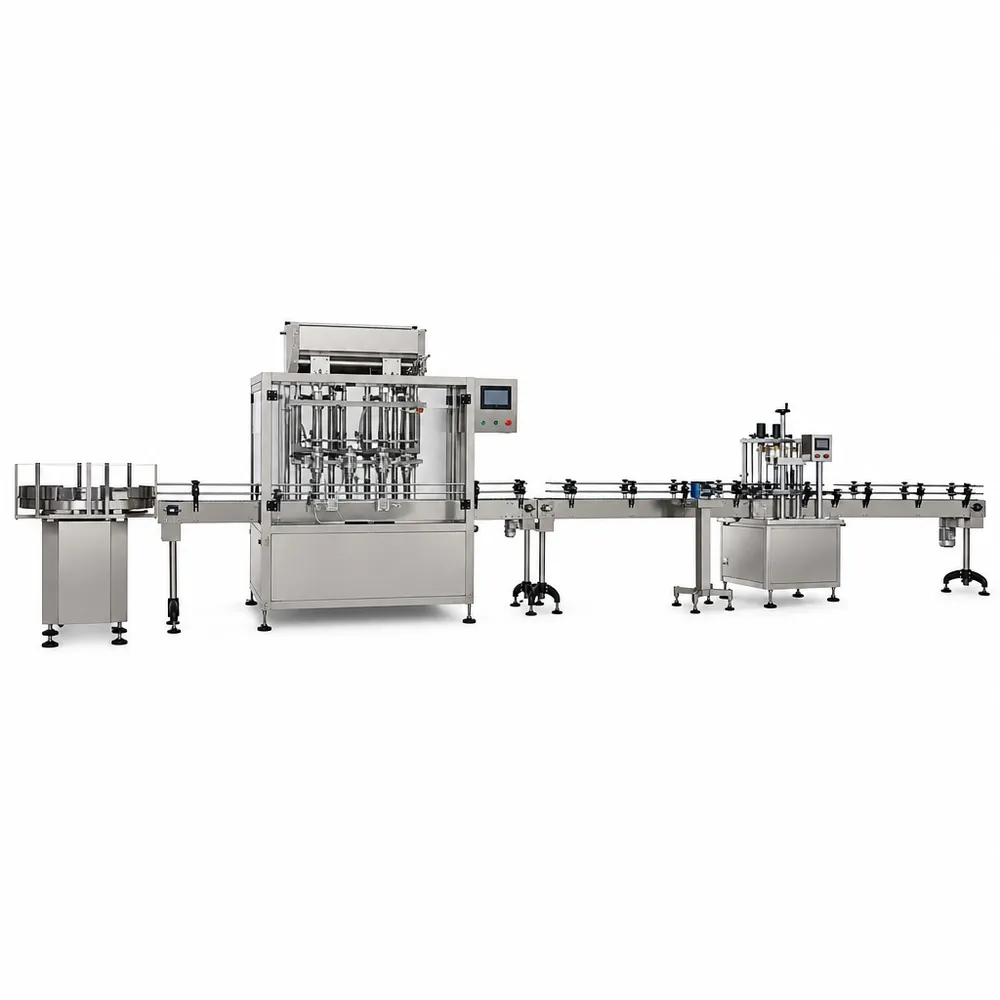
AT-02 combines servo piston filling with bottle feeding and capping in a line configuration.
View details →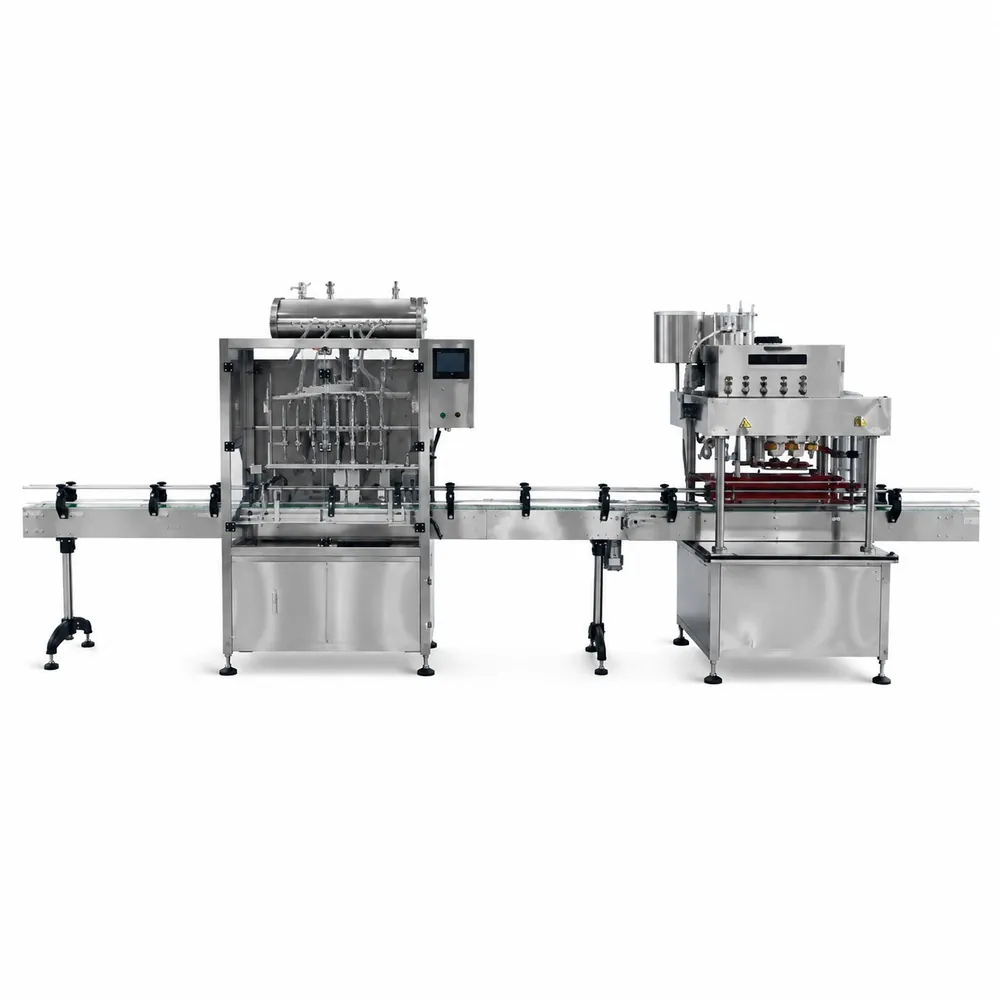
AT-03 uses vacuum-level filling for a matched bottle and liquid application. Filling / weighing range: 100mL-500mL.
View details →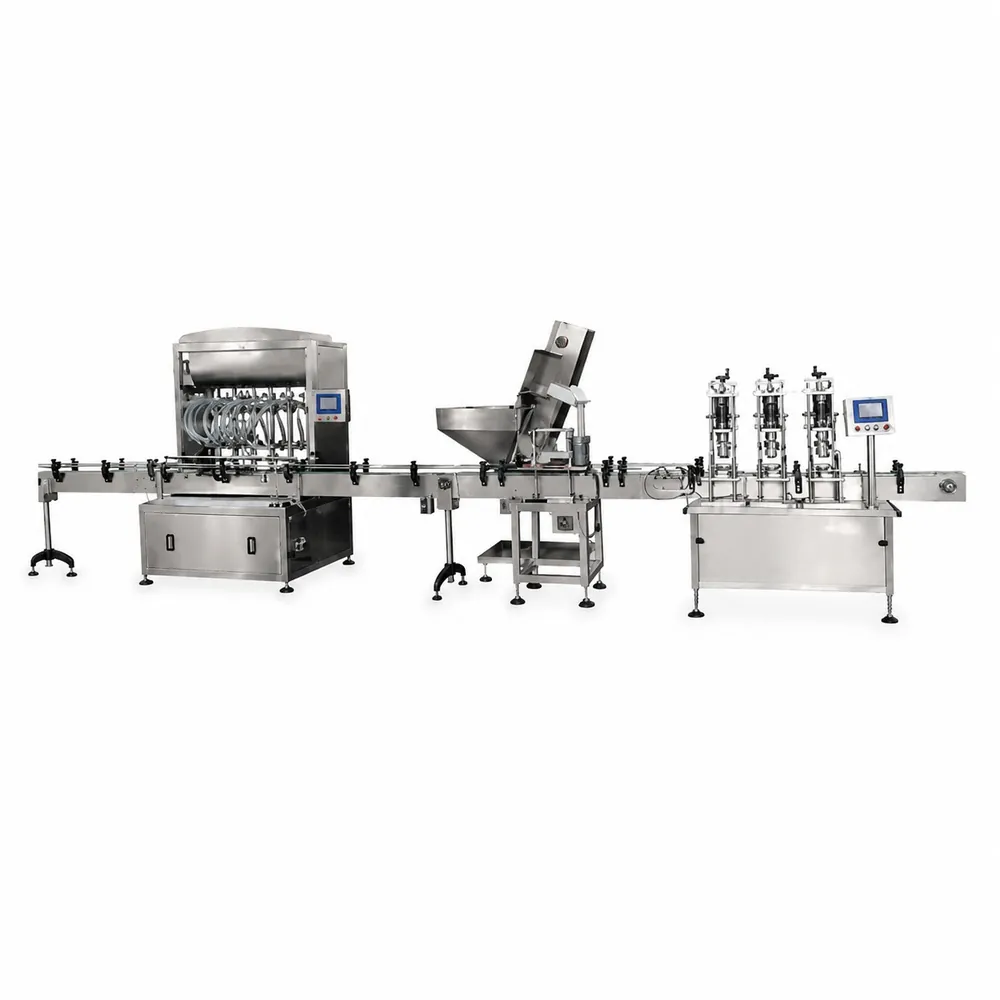
AT-04 is a sauce packaging line configuration covering bottle handling, filling, vacuum capping and labeling.
View details →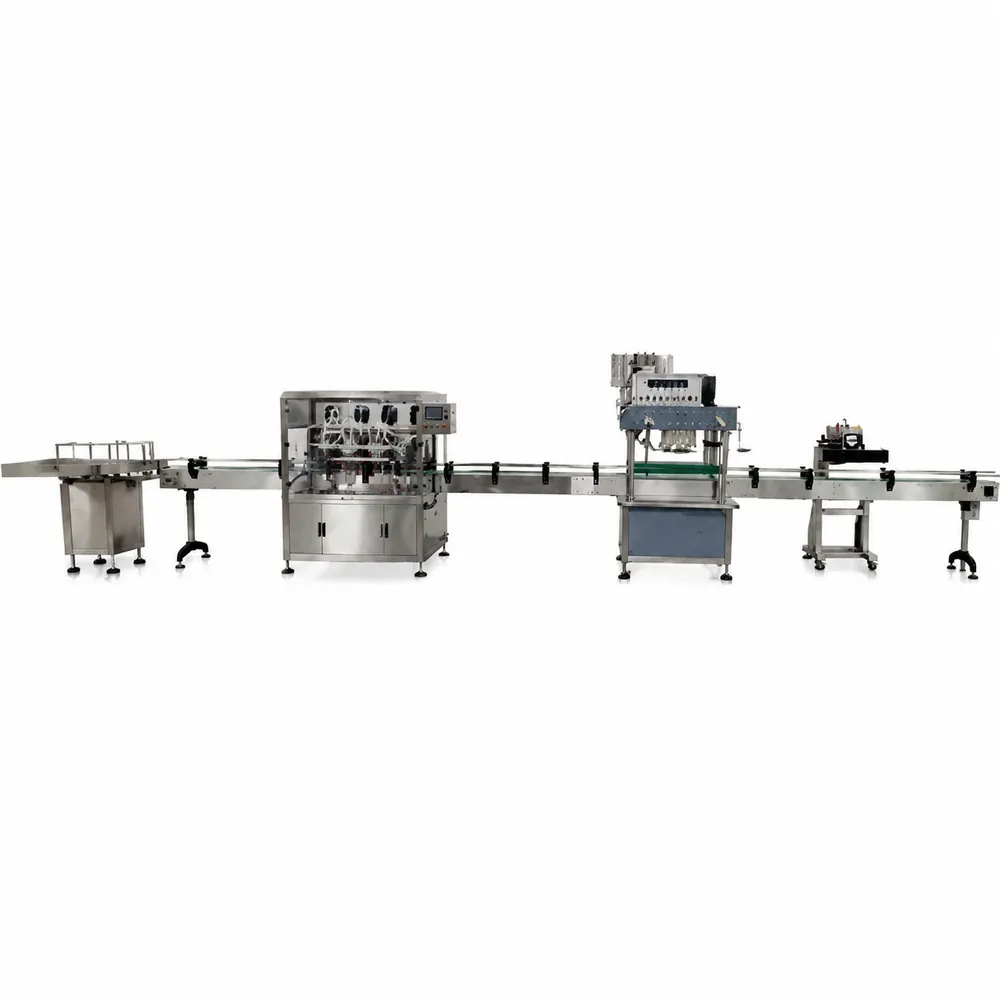
AT-05 is a peristaltic-pump filling and capping line. Filling / weighing range: 100–1000 mL.
View details →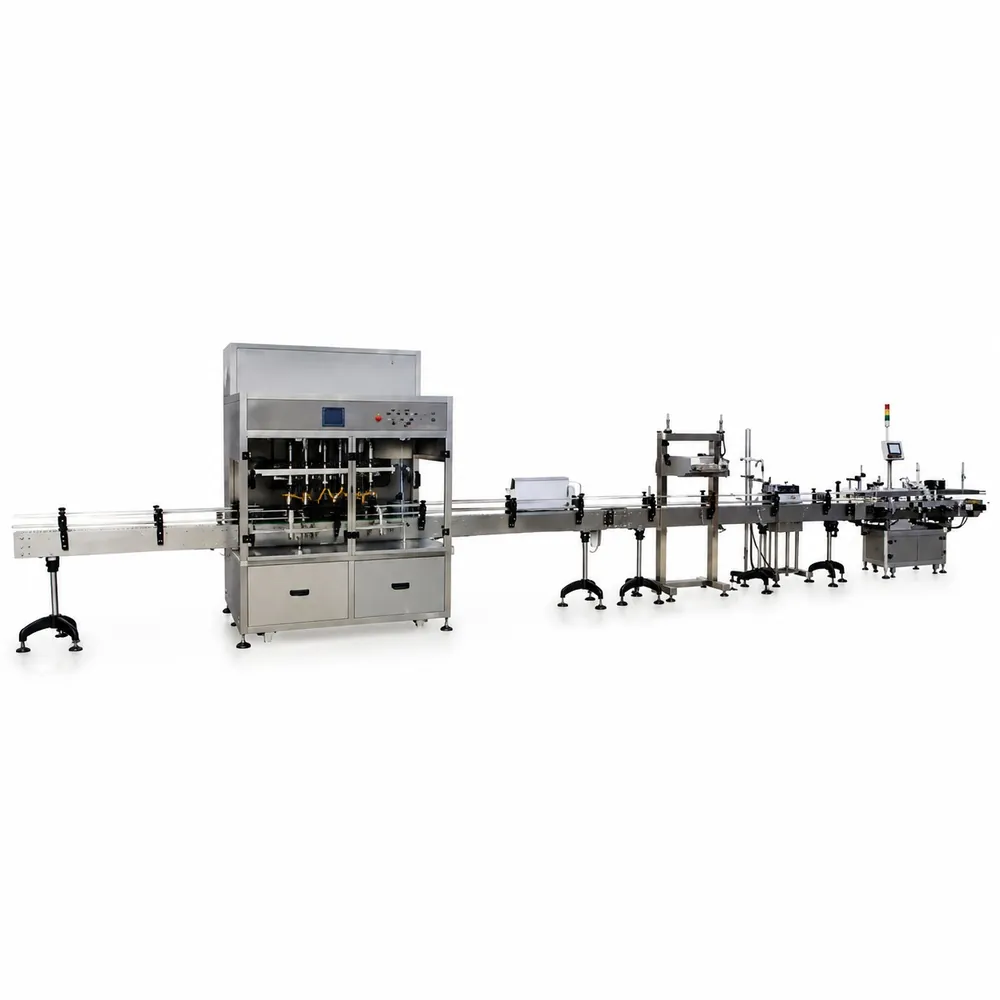
AT-06 is an edible-oil line configuration using flowmeter filling with bottle-handling, capping and labeling stages.
View details →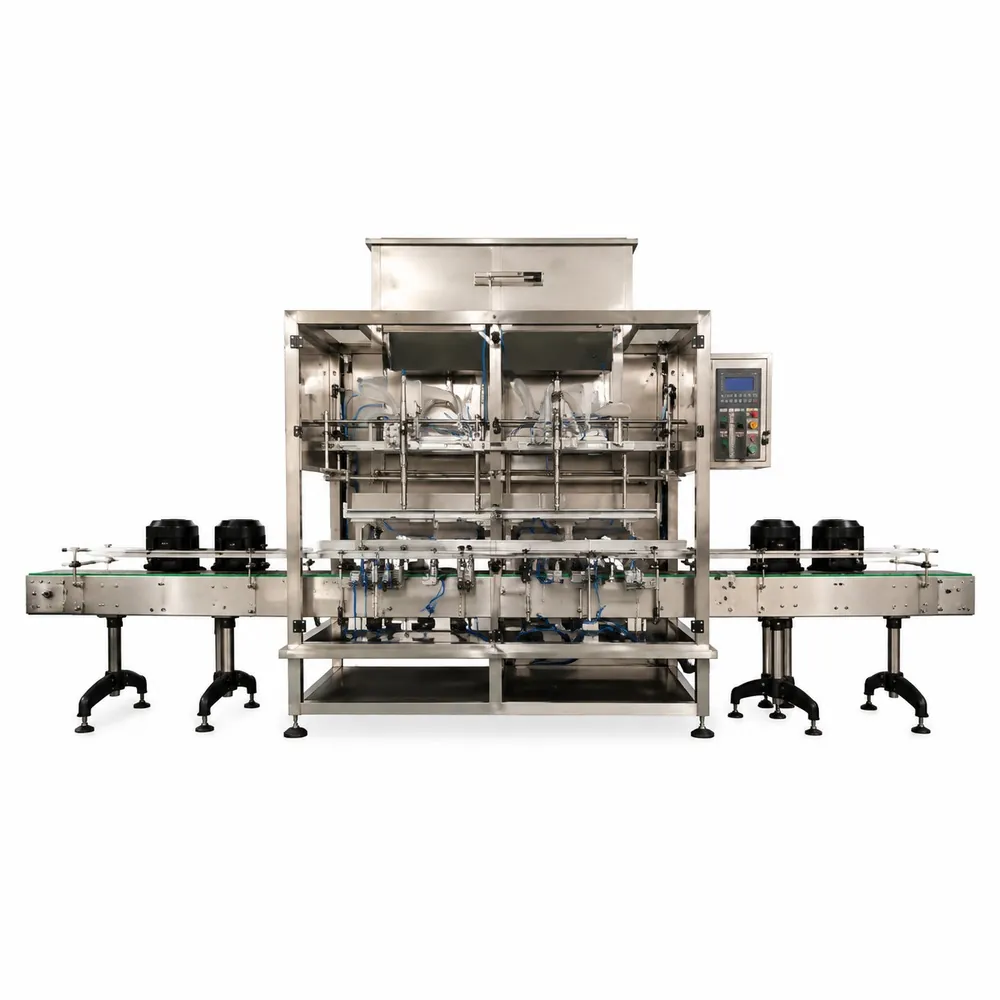
AT-2DGS-50L is a dual-head weighing liquid filling machine for a defined container and fill weight.
View details →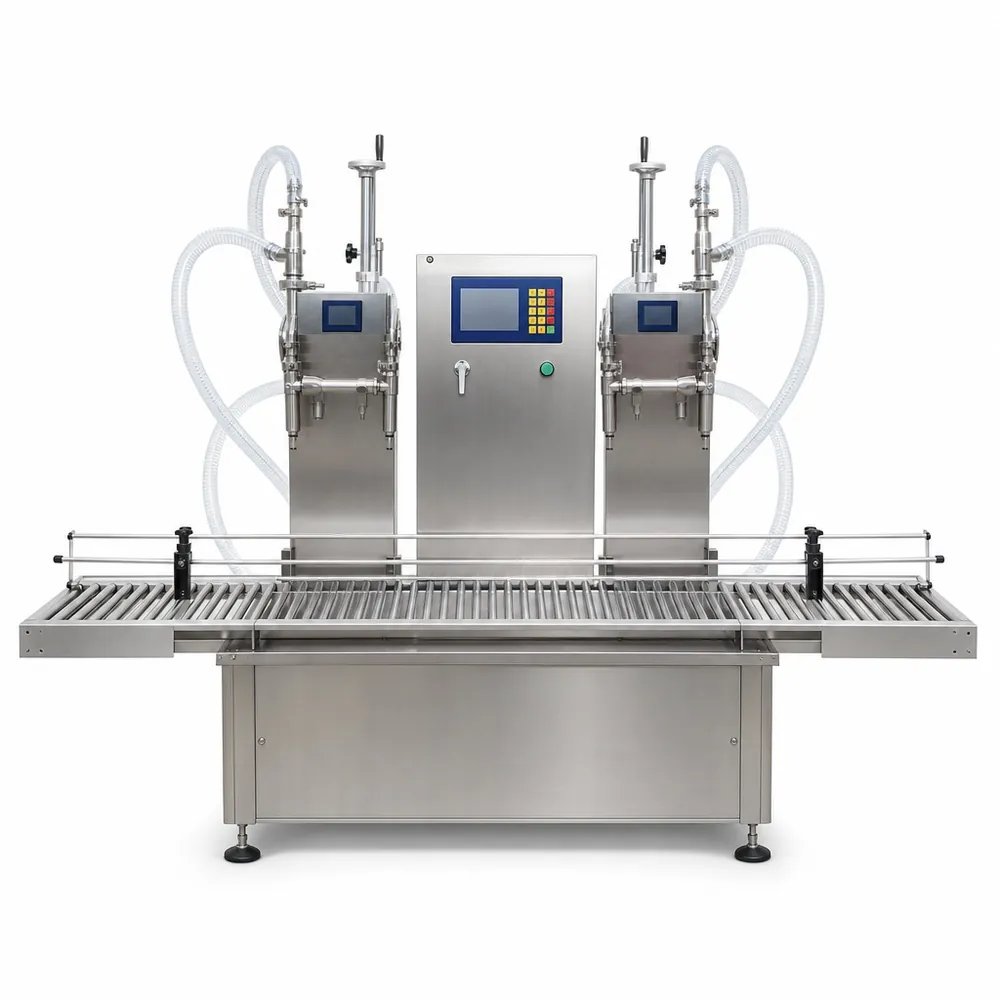
AT-2DGS-50Y uses two filling heads with weighing control for liquid filling. Filling / weighing range: 5kg – 50kg.
View details →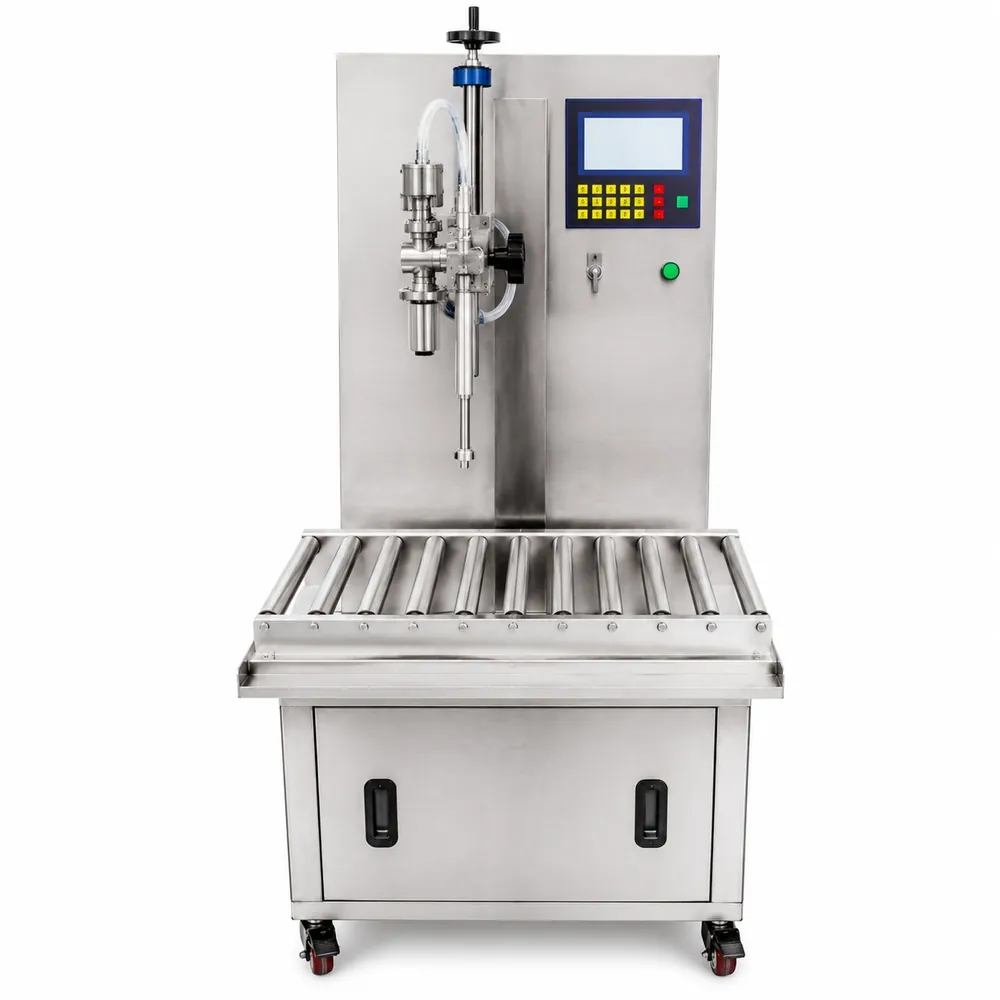
AT-DGS-50Y is a single-head liquid filler with weighing control. Filling / weighing range: 5kg – 50kg.
View details →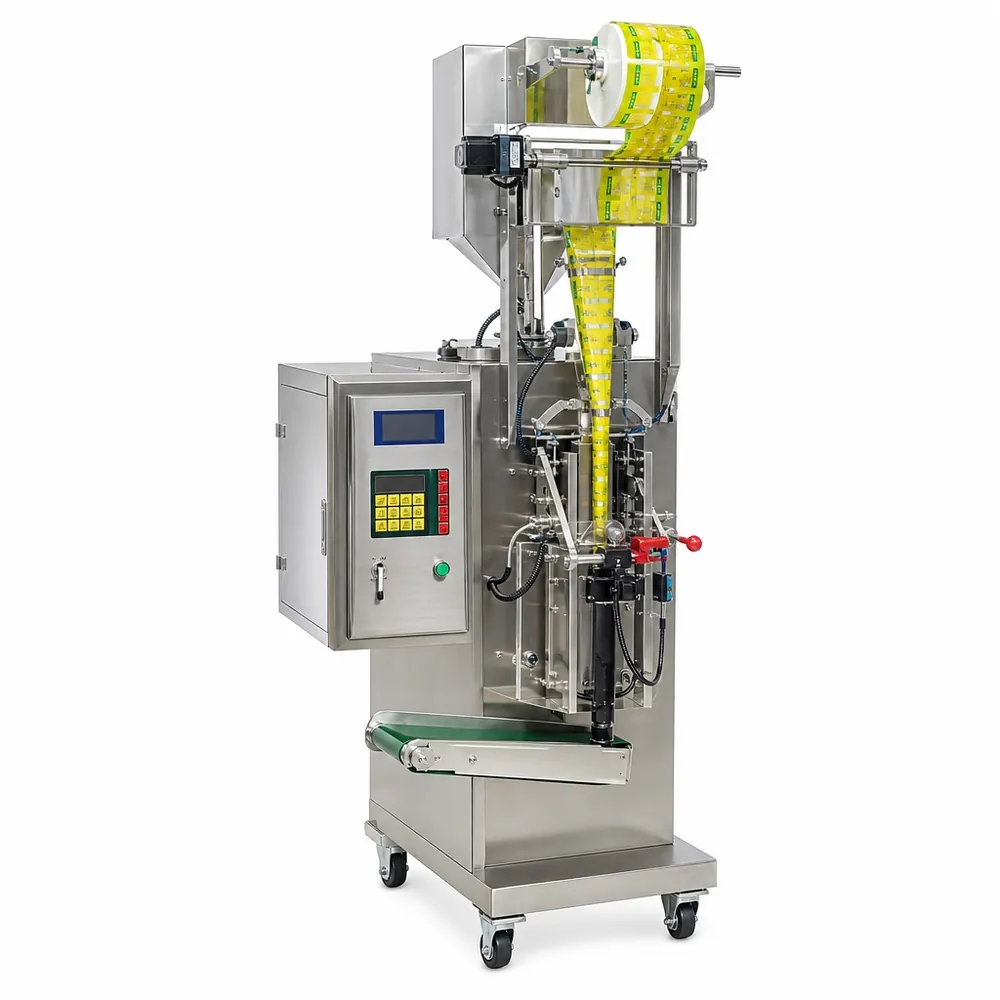
AT-DXDY uses piston dosing for liquid sachets. Filling / weighing range: 1–50 mL.
View details →Selection before specification
A compact line is a confirmed process boundary, not a bundle of machines. Define each station, interface and acceptance condition before choosing modules.
Selection guide
Share your material, package and output target to narrow the configuration.
List every included and excluded station from product infeed to accepted output.
Define line direction, transfer heights, accumulation, footprint, guarding and utilities.
Control each material, container, closure, label and package combination separately.
Define samples, accepted output, run window, documents, training and open-item closure.
Supply boundary
Common selection errors
Procurement FAQ
The stations need compatible product handling, speed coordination, transfer interfaces, controls, guarding, layout and a single acceptance boundary.
Provide the process sequence, formats, target output, room dimensions, line direction, utilities, operator access and included or excluded stations.
Use an agreed run window and count accepted packs after rejects, stops, replenishment and required operator actions are recorded.
Configuration input
Our team will use these details to recommend equipment for your application.